

| Contact Us |
| Name:colin |
| Email:colin@xhhjtech.com |
| T e l:+86 18602602237 |
Wrong Screw Breaks the Whole Line: Three Overlooked Selection Traps and On-Site Fixes
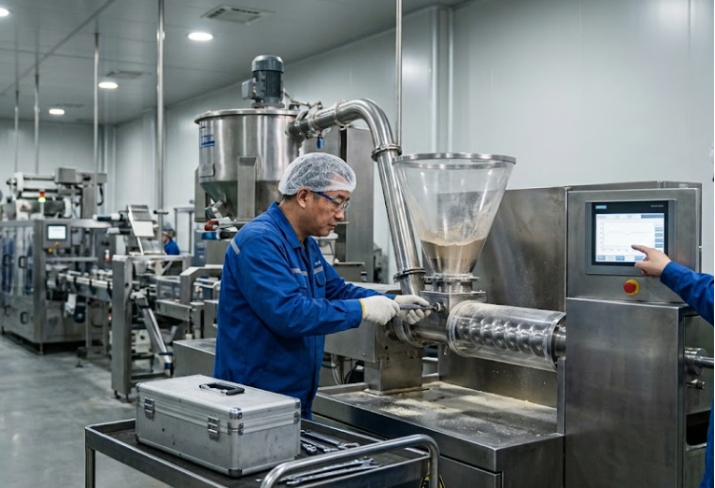
Many companies choose screw dosers based only on capacity, ignoring material properties. This often causes frequent failures after startup. The three most common selection mistakes are:
Mistake 1: No blow-back device for sticky materials
Powder sticks to the screw threads and builds up over time. This not only causes cross-contamination during product changes, but also changes the gap between the screw and the tube wall. As a result, the actual feed rate slowly drifts away from the set value without operators noticing.
Mistake 2: Ignoring the length-to-diameter ratio
For very fine dust-prone powders, if the screw is too short, material at the inlet can puff back due to an imbalance between screw thrust and gravity. Large amounts of dust blow back out of the hopper opening. This worsens the workshop environment and makes the actual feed rate much lower than the set value.
Mistake 3: Ignoring seal material
When feeding materials that contain organic solvents or are chemically corrosive, standard rubber seals can swell and deform quickly. In mild cases, this increases spindle resistance and causes motor current to spike. In severe cases, the screw can jam completely and stop the equipment.
If the doser suddenly delivers no material or far less than normal, follow this outside-in check sequence: First, check if the hopper is empty or if material has bridged to form a void. Next, look at the VFD panel for an overload alarm. Finally, check if the screw flight edges are worn and the gap to the tube wall is too large. When this gap exceeds the particle size, material will slip back in the screw channel and fail to move forward.
Remember, most equipment failures come from ignoring material properties during selection, and most shutdown problems can be prevented by weekly screw surface cleaning and monthly seal condition checks.


