

| Contact Us |
| Name:colin |
| Email:colin@xhhjtech.com |
| T e l:+86 18602602237 |
Negative-Pressure Feeding Station: 4 Key Details to Consider
Many powder-processing plants focus only on fan power and housing material when choosing a negative-pressure feeding station. In actual production, poor equipment design can lead to dust leakage, material loss, cross-contamination and hopper blockages.
The key is not simply suction power, but the internal chamber design.
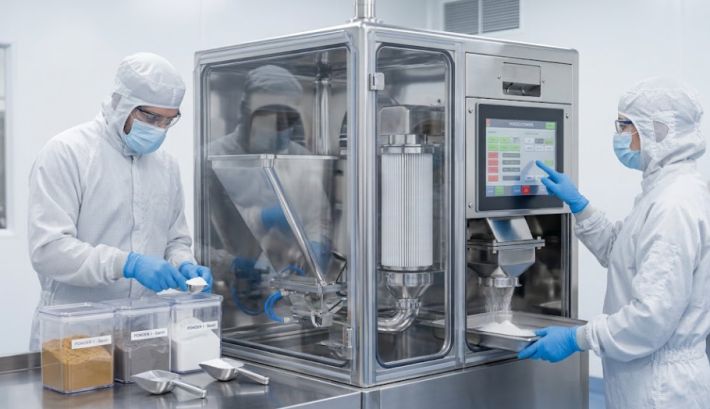
1. Independent Filter Chamber
A separate settling and filter chamber reduces direct powder impact on the filter and helps extend the life of PTFE-coated filter cartridges by 2–3 times, while reducing powder carryover.
2. Proper Hopper Design
A 60° hopper is suitable for sticky, moisture-sensitive powders. Light powders can be equipped with a pneumatic anti-bridging device to prevent blockages.
3. Quick-Release Design
A 316L mirror-polished chamber with tool-free quick release makes the hopper, screen and filters easy to remove and clean, helping prevent cross-contamination.
4. Integrated Functions
The feeding station can combine feeding, lump breaking, screening and metal removal, reducing equipment and floor-space requirements.
Common Selection Mistakes
1. Higher fan power is not always better. Excessive suction can increase powder loss and filter wear.
2. Do not focus only on the stainless-steel housing. Seals and filter-chamber materials must also meet food and pharmaceutical requirements.
3. One model cannot handle every powder. Different materials, such as pharmaceutical extracts, ultra-fine battery powdersand starch, require different hopper designs.


